Contact Us

Phone
08 8294 8664

Email
sale@awdmedical.com

Address

China Best Solid 27mm 3 Layer Yellow Formwork Panel Supplier

China’s construction sector continues to demand reliable, reusable panels for concrete projects. A Solid 27mm 3 Layer Yellow Formwork panel is designed for strength, stability, and repeated site use. Its three-layer structure can help resist bending under fresh concrete pressure. The yellow surface also improves panel visibility on busy jobsites.

Dr. Xie Qiang, a construction-formwork specialist, states, “Formwork quality is proven after stripping, not before pouring.” This practical view matters. A panel may look smooth in a warehouse. It must also remain stable during cutting, fixing, pouring, and removal. Good suppliers therefore inspect thickness, bonding, surface finish, moisture resistance, and edge sealing. They should provide clear product data, production records, and consistent export packaging.

Performance still depends on more than the panel itself. Poor support spacing can damage even strong plywood. Excessive vibration may cause surface defects. Releasing panels without proper cleaning can shorten their service life. These details are often overlooked. That assumption needs correction.

A dependable Chinese supplier should understand project conditions, not only quote a low price. Buyers may need samples, loading guidance, customization, and technical communication. Factory experience is useful, but honest limitations matter too. No formwork panel performs perfectly in every climate or application. Storage conditions, concrete mix, and workmanship remain important.

For contractors, the right Solid 27mm 3 Layer Yellow Formwork panel can support cleaner concrete faces and more predictable scheduling. Careful supplier evaluation creates the real advantage. Not the color alone.

China Best Solid 27mm 3 Layer Yellow Formwork Panel Supplier

Product Overview and Key Features of 27mm Three-Layer Yellow Formwork Panels

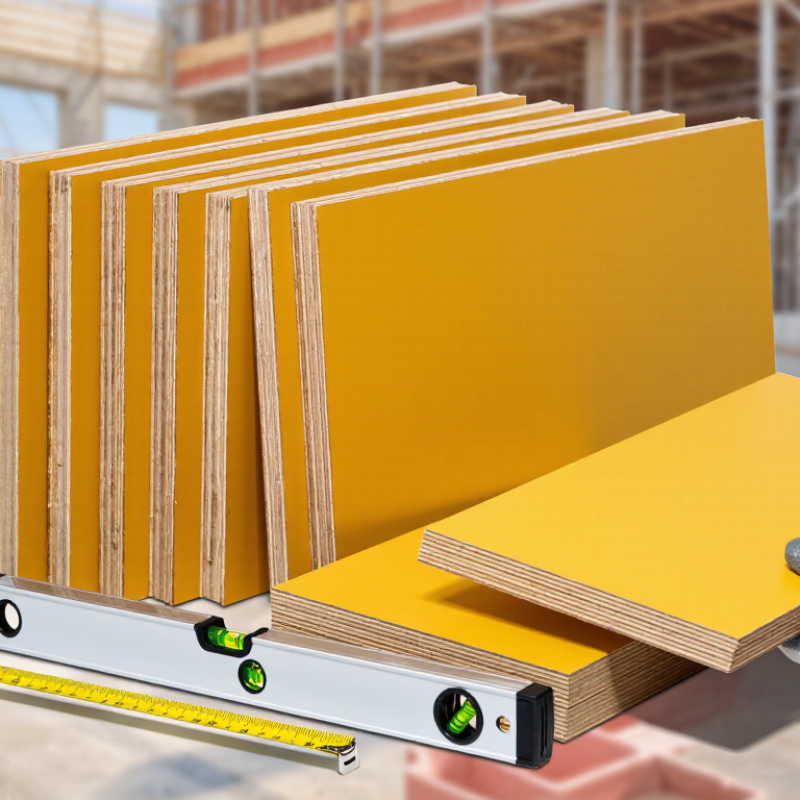
27mm three-layer yellow formwork panels are built for repeated concrete casting in walls, columns, and slabs. Their solid timber structure provides a firm working surface and supports stable panel alignment. At 27 mm, the board balances load capacity with manageable handling on busy sites. The yellow film makes surface contamination, cuts, and edge damage easier to notice. That helps supervisors inspect panels before installation. Small defects matter.

The three-layer design should show even bonding, smooth faces, and sealed edges. A capable supplier should provide thickness tolerance, moisture data, bonding information, and test records. These details support professional purchasing decisions. Moisture control is especially important because swollen cores can affect concrete finishes and panel joints. Inspect the corners carefully. Edge sealing reduces water entry, but it cannot replace proper storage. Keep panels raised from wet ground and covered without trapping condensation. In practice, reuse life depends on cleaning, release-agent application, cutting quality, and handling habits. Do not trust optimistic reuse figures alone. A careful supplier explains expected performance under defined conditions and accepts that site results may vary. After stripping, remove concrete residue with suitable tools, not aggressive impacts that damage the film. Manufacturers and contractors should review failed panels, because small installation mistakes often reveal larger process weaknesses.

27mm Three-Layer Yellow Formwork Panel: Product Overview

This specification chart highlights the two core structural characteristics identified for the panel: a nominal total thickness of 27 mm and a three-layer construction. The yellow surface is a visual product characteristic and is not represented as a numerical performance value.

Core Materials and Three-Layer Panel Construction

China Best Solid 27mm 3 Layer Yellow Formwork Panel Supplier

A 27mm three-layer formwork panel depends on its core, not only its yellow surface. Typical cores use poplar, eucalyptus, or mixed hardwood veneers. Each layer should run across the next, improving load distribution and reducing splitting. The face film normally uses resin-impregnated paper over a smooth wood surface. It helps resist concrete moisture, abrasion, and release-agent chemicals.

The USDA Forest Products Laboratory’s Wood Handbook reports approximately 12% equilibrium moisture content at 20°C and 65% relative humidity. This figure matters during storage and production. Excess moisture can swell the core and reduce panel stability. EN 636 and EN 314-2 also emphasize structural plywood performance and bonding quality. Therefore, buyers should request veneer thickness, adhesive class, density, and water-boil test results. A uniform yellow finish proves little. I would not promise high reuse numbers without checking concrete pressure, cutting, edge sealing, and cleaning practice.

Tips: Store panels flat and raised from the ground. Seal every cut edge quickly. Inspect corners before each pour. A small void can grow. Measure thickness across several points, not one. The Forest Products Annual Market Review also shows continued pressure on wood-product supply and pricing, so responsible sourcing and batch traceability deserve attention. Three layers can perform well, but poor bonding still defeats the design.

Manufacturing Process and Quality Control Standards

A reliable 27mm, three-layer yellow formwork panel begins with controlled raw materials. Veneers are peeled, clipped, and dried to a target moisture content of 8–12%. Operators check each sheet for open knots, splits, and uneven thickness. The core layers are cross-oriented to reduce warping. Phenolic adhesive is applied by calibrated rollers, not visual judgment. Hot pressing then follows a recorded pressure, temperature, and time schedule. Typical production targets use 120–140°C, but the exact cycle depends on wood species and adhesive chemistry.

Quality control must continue after pressing. Each batch should receive thickness, squareness, moisture, bonding, and surface inspections. A practical internal target is ±0.5mm thickness tolerance, supported by calibrated gauges and retained samples. Bond performance can be evaluated against EN 314-2 requirements, while formaldehyde emissions should follow EN 717-1 testing procedures. ISO 9001:2015 also supports traceability from veneer receipt to final packing. The UNECE/FAO Forest Products Annual Market Review 2023–2024 highlights continuing volatility in wood-panel supply and production costs, making documented inspection more important. A low price may hide weak glue spread or rushed drying. That risk deserves attention. Even a bright yellow surface can look perfect while internal bonding remains inconsistent. Suppliers should test panels after conditioning, not only immediately after pressing.

China Best Solid 27mm 3 Layer Yellow Formwork Panel Supplier - Manufacturing Process and Quality Control Standards
Typical technical specification and factory quality-control data for a reusable 27 mm, three-layer, yellow film-faced plywood formwork panel
Category Data Dimension Typical Specification or Quality Requirement Manufacturing and Inspection Method
Product Structure Panel type Three-layer structural plywood panel with balanced face, core, and back veneers. Veneer grains are arranged with adjacent layers cross-bonded to improve dimensional stability. Review production drawings and verify the number and orientation of veneer layers during lay-up.
Product Structure Nominal thickness 27 mm, with a typical finished thickness tolerance of approximately ±0.5 mm, subject to the agreed product specification. Measure with a calibrated digital thickness gauge at multiple points on every inspection batch.
Product Structure Common panel dimensions Typical production sizes include 1,220 × 2,440 mm and 1,250 × 2,500 mm. Custom dimensions may be produced according to the construction project requirements. Check length, width, squareness, and edge straightness before film application and final packing.
Raw Materials Veneer species Rotary-cut hardwood or mixed hardwood veneers with uniform thickness, adequate density, and no active decay, insect damage, or excessive loose knots. Incoming visual grading, veneer thickness measurement, moisture inspection, and rejection of defective sheets.
Raw Materials Veneer moisture content Typical target range: 8%–14% before adhesive application. The selected range should be compatible with the adhesive system and local climate. Use a calibrated wood moisture meter; record readings by batch and storage location.
Manufacturing Process Veneer preparation Veneers are peeled, clipped, dried, graded, and repaired where permitted. Sheets should be flat enough to achieve continuous adhesive contact. Inspect veneer thickness, surface cleanliness, flatness, defects, and repair quality before gluing.
Manufacturing Process Adhesive system Exterior-grade phenolic or melamine-urea-formaldehyde adhesive may be used. Adhesive selection must provide moisture-resistant bonding suitable for repeated concrete-forming exposure. Verify adhesive type, mixing ratio, viscosity, storage life, application rate, and batch traceability.
Manufacturing Process Glue spreading Uniform adhesive coverage is required on the bonding surfaces. The controlled spread rate is normally established through the adhesive supplier's technical data and production trials. Check spread rate by weighing test samples and inspect for dry areas, puddling, and uneven application.
Manufacturing Process Lay-up and pre-pressing The three veneer layers must be aligned, cross-oriented, and pre-pressed sufficiently to prevent shifting, open joints, and edge separation. Confirm grain direction, panel alignment, joint arrangement, pre-press pressure, and pre-press holding time.
Manufacturing Process Hot pressing Pressing temperature, pressure, and time are controlled according to the adhesive formulation, veneer moisture, and panel thickness. The full panel must achieve consistent curing. Record press temperature, pressure, closing time, curing time, and platen condition for each production batch.
Surface Treatment Yellow film facing Both faces are normally covered with a smooth yellow phenolic film. Common film weights are approximately 120–240 g/m² per face, depending on the required reuse level and surface finish. Verify film weight, color uniformity, surface cleanliness, film alignment, and absence of wrinkles or blisters.
Surface Treatment Film lamination The film should be fully bonded to the plywood surface without visible peeling, edge lifting, bubbles, folds, or unbonded areas. Visual inspection, edge inspection, and periodic adhesion or boiling-water exposure testing according to the agreed test plan.
Machining Edge trimming Edges should be clean, straight, and free from major splinters, delamination, and missing corners. Cut edges should be sealed when required for enhanced moisture resistance. Inspect all four edges and use a straightedge and squareness tool for dimensional verification.
Dimensional Control Length and width tolerance Typical commercial tolerance is approximately ±1 mm for standard panel dimensions, unless a project-specific tolerance is agreed. Measure with a calibrated steel tape or digital measuring system at final inspection.
Dimensional Control Squareness and diagonal difference The panel should remain square, with the difference between the two diagonals commonly controlled to approximately 2 mm or less for standard-size panels. Measure both diagonals and compare the result with the approved inspection specification.
Physical Properties Finished-panel moisture content Typical release range: 8%–14%, with no localized wet areas or abnormal moisture gradients. Take readings at the face, center area, and edges of sampled panels.
Physical Properties Density consistency The panel should have uniform density without large resin pockets, hollow areas, severely compressed zones, or visibly weak core sections. Density is commonly evaluated by batch rather than by a single universal value. Determine density from panel mass and volume on sampled units; combine with visual and internal-bond inspection.
Bonding Quality Bonding classification For exterior formwork exposure, the bonding performance should be suitable for exterior-use plywood. EN 314-2 Class 3 is a commonly referenced bonding classification where applicable. Conduct glue-line shear testing according to EN 314-1 and evaluate against the applicable requirements of EN 314-2 or the project standard.
Bonding Quality Delamination resistance No significant glue-line opening, veneer separation, or film lifting should occur after the specified water-resistance test. Use boiling-water or cyclic water-exposure testing according to the selected standard and approved inspection plan.
Mechanical Quality Bending performance Bending strength and modulus depend on veneer species, grain direction, density, and construction. Values should be confirmed by a laboratory test report rather than assumed from thickness alone. Perform bending tests in the principal directions using EN 310, ASTM D3043, or another contractually agreed method.
Surface Quality Concrete-facing surface The yellow film should be smooth and continuous, without visible pinholes, deep scratches, contamination, open film joints, or areas likely to imprint on concrete. Inspect under consistent lighting before packing; classify defects according to approved visual samples.
Chemical Safety Formaldehyde emission For markets requiring an E1 classification, formaldehyde emissions should comply with the applicable limit, commonly assessed by EN 717-1. The declared class must be supported by a valid test report. Use periodic third-party or in-house laboratory testing with traceable samples from production batches.
Quality Inspection Sampling plan A practical inspection plan includes 100% visual inspection for major surface and edge defects, with dimensional and performance tests performed on representative samples. Apply an agreed AQL or project-specific sampling plan; retain inspection records and test specimens.
Traceability Batch identification Each production batch should be traceable to veneer preparation, adhesive batch, pressing cycle, film batch, inspection results, and packing date. Use batch numbers on inspection records, labels, pallets, and quality certificates.
Packaging Pallet protection Panels should be stacked on level supports, protected from direct rain and ground moisture, and secured to prevent edge damage, sliding, and excessive bending during transport. Inspect pallet alignment, protective wrapping, corner protection, strapping, labels, and loading condition.
Storage and Use Recommended storage condition Store horizontally on level supports in a covered, ventilated area. Avoid direct sunlight, standing water, and rapid changes in temperature or humidity. Check warehouse conditions and confirm that panels are not stored directly on the floor or exposed to weather.
Compliance Reference standards Common reference documents include EN 636 for plywood performance, EN 314-1 and EN 314-2 for bonding quality, EN 310 for bending properties, EN 322 for moisture content, EN 315 for dimensional tolerances, and EN 717-1 for formaldehyde emission testing. The applicable standard, edition, test frequency, and acceptance limits should be stated in the purchase specification or quality agreement.
Release Criteria Final acceptance Accept: correct thickness and dimensions, sound three-layer construction, fully bonded film, acceptable appearance, compliant moisture content, satisfactory test results, and complete traceability documentation. Quality manager approval based on final inspection records, laboratory results, and customer-specific requirements.
Note: The numerical values shown are typical production targets or commonly used inspection ranges for 27 mm three-layer film-faced formwork plywood. Final acceptance limits should be confirmed against the applicable national standard, project specification, testing method, and intended construction use.

Applications and Performance Benefits in Concrete Formwork

Solid 27mm three-layer yellow formwork panels support demanding concrete applications, especially walls, columns, slabs, and repeated modular pours. The Global Cement and Concrete Association estimates that the world produces about 14 billion cubic metres of concrete annually, creating constant demand for stable, reusable formwork. A 27mm panel offers practical stiffness while remaining manageable on busy construction sites.

The yellow surface helps crews identify panels quickly and inspect damage before installation. Smooth faces matter. They can reduce surface blemishes, simplify stripping, and limit concrete paste absorption when edge sealing and release agents are used correctly. The three-layer structure distributes pressure more evenly than thin, poorly balanced sheets. However, performance depends on framing spacing, tie design, moisture exposure, and storage. A stronger panel cannot correct weak supports.

ACI 347R-14, Guide to Formwork for Concrete, requires formwork to resist concrete pressure, construction loads, and expected movement. OSHA 29 CFR 1926.703 also requires formwork to support anticipated vertical and lateral loads safely. In field use, careful handling often determines service life more than color or thickness. Panels should be stacked flat, kept off wet ground, and inspected after every pour. Some suppliers overstate reuse cycles; actual results vary. That point deserves honest measurement, not optimistic marketing.

How to Choose a Reliable Formwork Panel Supplier in China

China Best Solid 27mm 3 Layer Yellow Formwork Panel Supplier

Choosing a reliable formwork panel supplier requires more than comparing prices. Check the supplier’s production records, quality system, and export experience. A solid 27mm, three-layer yellow panel should have consistent thickness, sealed edges, and smooth film bonding. Ask for recent test reports covering water absorption, bending strength, and formaldehyde emissions. These details affect stripping time and concrete surface quality.

McKinsey Global Institute reported that construction productivity grew about 1% annually over two decades, compared with 2.8% across the wider economy. Better material coordination can reduce this gap. A dependable supplier should confirm panel dimensions, pallet protection, loading photos, and delivery schedules in writing. Request samples from current production, not only showroom pieces. Inspect the core layers carefully. Small voids can become expensive defects. A low quotation may hide inconsistent glue application or weak edge sealing.

Tips: Compare at least three suppliers. Verify factory capacity through a live video inspection or independent audit. Ask how rejected panels are recorded and replaced. Confirm whether the supplier can provide batch numbers and inspection data. Do not judge yellow panels by color alone; surface flatness and bonding quality matter more. A supplier may pass a basic inspection and still perform poorly during repeated use. That is where careful trial orders become valuable. ISO Survey 2022 recorded more than one million ISO 9001 certificates worldwide, but certification alone cannot prove product consistency. Check the evidence behind it.